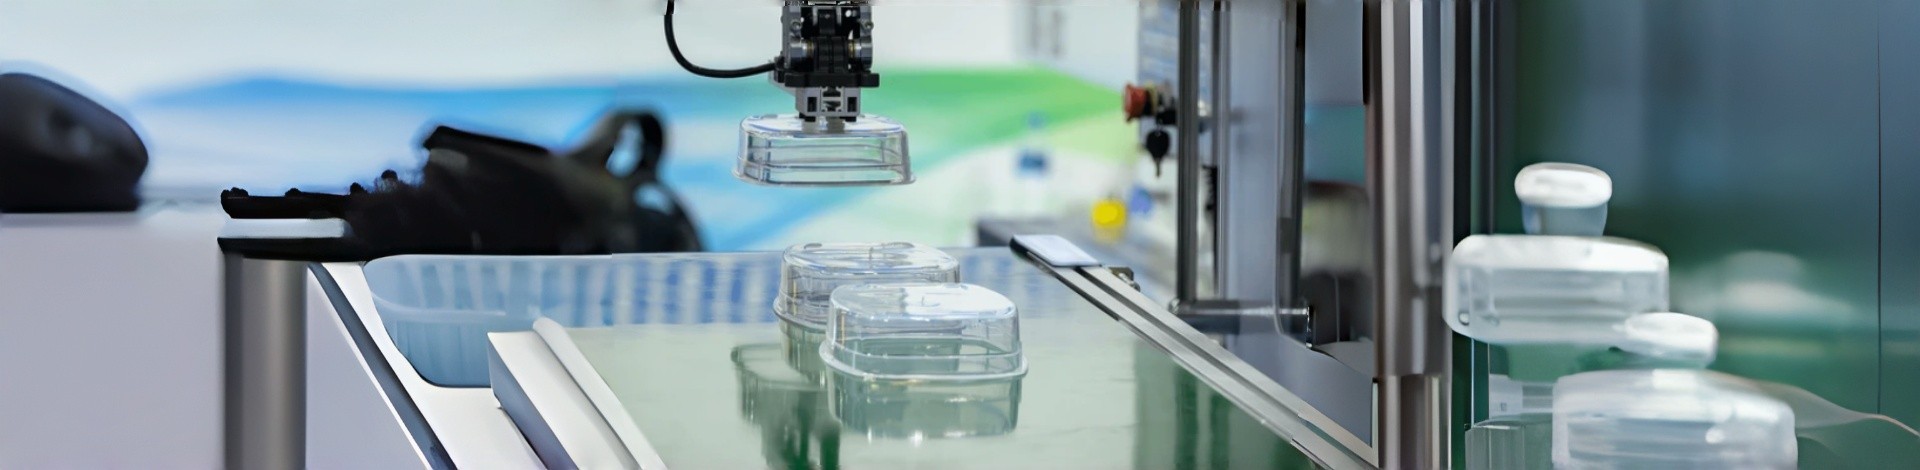
Injection molding
For injection molded parts, the core basis for acceptance is the drawing. However, the characteristics of plastics mean they follow a judgment logic different from metal processing.
1. Dimensional Accuracy
Dimensions with tolerances specified on the drawing must pass. For dimensions without specified tolerances, the tolerance grades in GB/T 14486 (China) or ISO 20457 (international) are usually referenced. ISO 20457 is specifically developed for plastic molded parts and takes into account plastic-specific factors such as shrinkage and warpage. The tolerance approach for metal parts cannot be directly applied.
One point requires special attention: injection molded parts continue to change in size after demolding. Residual stress release and post-crystallization both cause further dimensional shifts. Therefore, measurements should be taken at least 24 hours after demolding. Otherwise, the data obtained will not reflect the final state.
2. Geometric Tolerances
Warpage and deformation in injection molded parts are more common than dimensional out-of-tolerance, and harder to correct. Geometric tolerance items such as flatness, coaxiality, and position tolerance directly reflect the degree of deformation of the product. For assembly surfaces and sealing surfaces, geometric tolerances are often more decisive than dimensional tolerances.
3. Appearance Quality
The core principle of appearance acceptance is differentiated treatment by surface. Product surfaces are usually classified as A surface (primary visible surface), B surface (side surface), C surface (bottom/back surface), and D surface (internal). Acceptance standards vary greatly between different surfaces: an A surface may require "no visible defects to the naked eye," while a C surface allows minor imperfections that do not affect function.
Common defect evaluation items include: sink marks, flash, weld lines, color difference, bubbles, and silver streaks. Flash height is typically required to be ≤0.1mm, and color difference ΔE ≤1.5.
0086 0755 23170739
0086-0755-24325235
ciky@hainamould.com
Room 1605, 16th Floor, Hongyu Building, No. 495, Donghuan 2nd Road, Longhua Subdistrict, Longhua District, Shenzhen, Gongdong ,China 518109


Copyright 2026 Hainamould.com All rights reserved.
-
 0086 0755 23170739
-
 Facebook
-
 WhatsApp
-
 LinkedIn
-
 TOP